Key takeaway
- How computer vision inspects assembly lines: pipeline, imaging options, edge vs cloud, ISO and EU AI Act checks, and a staged adoption plan.
A computer vision inspection system on an assembly line photographs each part or assembly, runs a trained model on the image and tells the line to pass, reject or rework it. It earns its place when defects are small, products change often or the line is too fast for people to check every unit. It works only if the cameras, lighting, labelled data and the decision rules around the model are treated as one engineered system.
This guide is for CTOs, heads of manufacturing technology and solution architects. It covers how an inspection pipeline is built, which inspection tasks suit vision, where the model should run (see our guide to computer vision on edge), which standards apply and how to adopt it in stages. Inspection here means checking made parts; for screening video content, see AI-powered video analytics.
What does computer vision do on an assembly line?
Cameras and sensors capture images of products as they move. A model compares each image with what a good part looks like, finds defects, missing parts, wrong positions or unreadable labels, and sends a result to the line controller. Our wider overview of computer vision applications covers other uses; this post stays on the inspection station.
Treat vision as a quality-control step inside a quality management system. ISO 9001:2015, according to ISO's own page, sets generic requirements for a quality management system that helps an organisation deliver products and services meeting customer and legal needs and supports continual improvement. An inspection result is useful when it feeds that improvement loop, not only a reject bin.
How does an automated inspection pipeline work?
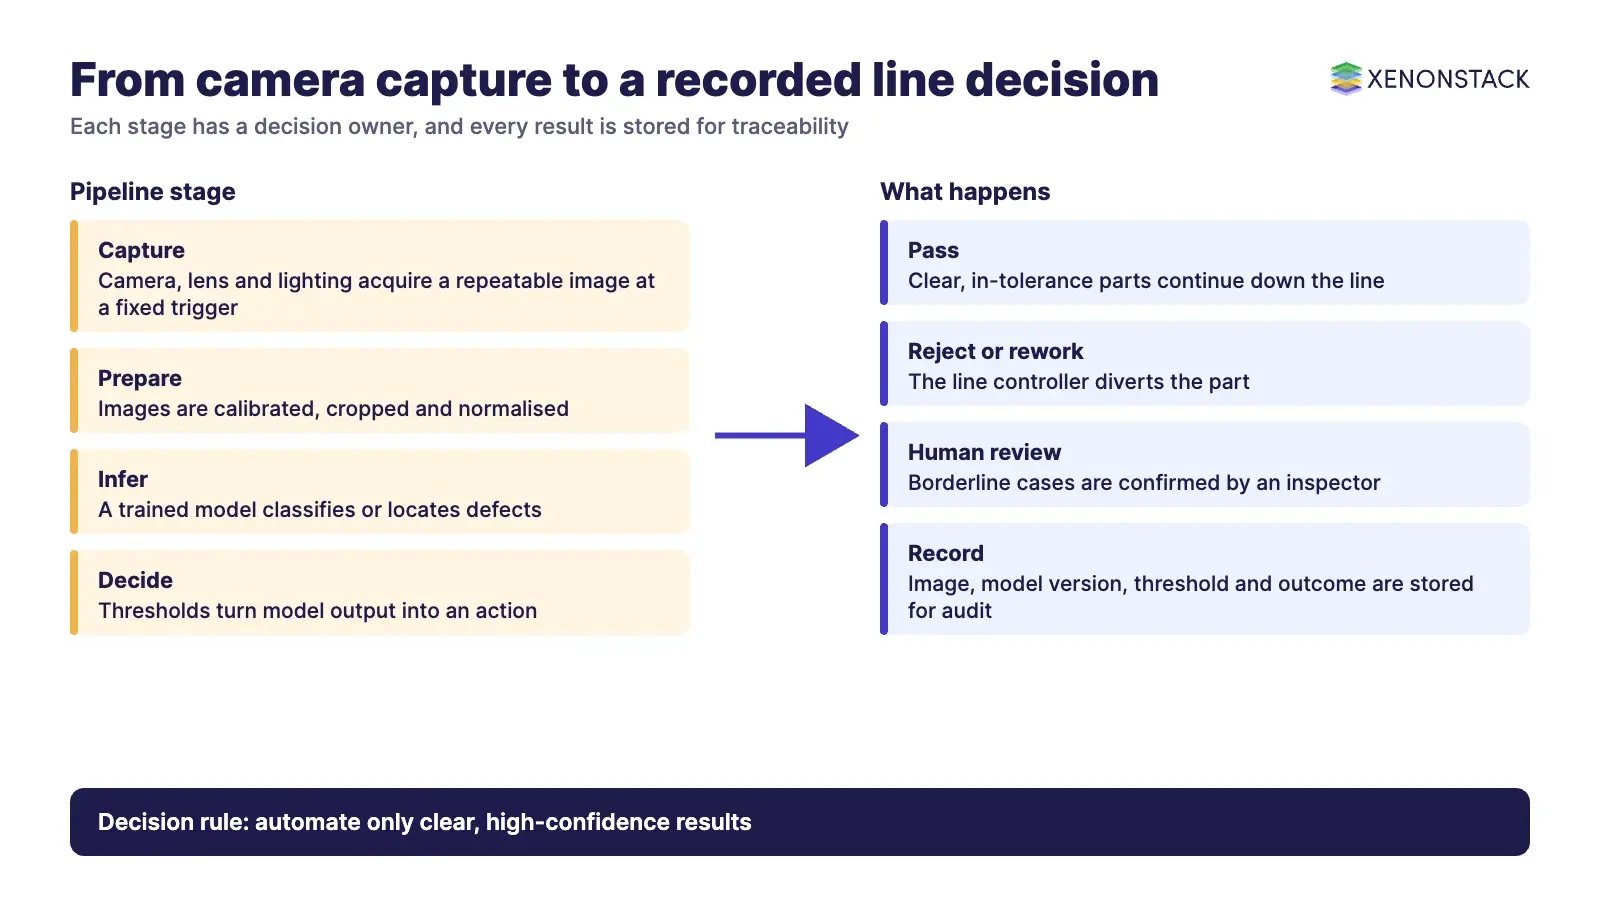
| Stage | What happens | What to decide |
|---|---|---|
| Capture | Camera, lens and lighting acquire a repeatable image at a fixed trigger point | Resolution, lighting, trigger and fixturing |
| Prepare | Images are calibrated, cropped and normalised; OpenCV, according to its documentation, provides modules for image processing (imgproc) and camera calibration (calib3d) | Calibration routine and tolerance for drift |
| Infer | A trained model classifies or locates defects | Which model, and where it runs |
| Decide | Rules turn model output into pass, reject, rework or review | Thresholds, and who owns them |
| Act and record | The line controller diverts the part; the result and image are stored | Retention, traceability and feedback to training data |
Which technologies matter most for inspection?
Convolutional networks and vision transformers are the usual model families for classifying and locating defects; see our note on vision transformers. Beyond the model, the imaging choice often decides what can be seen at all.
| Technique | Good for | Watch out for |
|---|---|---|
| 2D area-scan imaging | Surface marks, presence or absence, label and code reading | Lighting changes and reflective surfaces |
| 3D vision (stereo, structured light, LiDAR) | Height, flatness, volume and shape errors; see 3D vision and depth estimation | Calibration effort and cycle time |
| Multispectral and hyperspectral imaging | Material differences the eye cannot see | Cost, data volume and specialist set-up |
| Explainable outputs | Showing operators which region triggered a reject | Heat maps are an aid for review, not proof of correctness |
Which inspection tasks suit computer vision?
| Task | Typical example | When it fits |
|---|---|---|
| Defect detection | Solder joints, scratches, dents, missing parts | Defects are visible and you can collect labelled examples |
| Assembly verification | Correct parts, orientation and sequence | The correct state is well defined |
| Dimensional measurement | Gaps, hole positions, part size against drawing | You can calibrate the camera and control fixturing |
| Surface inspection | Discolouration or uneven coating | Lighting is controlled |
| Code and label checks | Barcode, QR code and label legibility | Codes pass on a fixed route |
| Worker and equipment safety | Presence of people near automated equipment | Treat it as a monitoring aid; safety functions need certified safety systems |
Vision can also watch machines for visible wear and misalignment, which supports maintenance planning. Treat it as one input beside vibration and temperature data, not a replacement.
Where should the inspection model run?
Running inference next to the line keeps latency low and keeps images on site; training and fleet management often sit in the cloud. Our guides to AI solutions for edge devices and AI vision models on Intel AI accelerators cover hardware choices, and edge AI in smart factories covers the factory context. For running such workloads across on-premises, cloud and hybrid sites, NexaStack is described on its site as an agentic operating platform for physical AI that runs across on-premises, cloud and hybrid environments. XenonStack's edge and vision AI platform describes lightweight agents on local devices for real-time video analysis.
What are the main challenges and how are they handled?
| Challenge | Practical response |
|---|---|
| Too few labelled defect images | Collect from the line over time; use transfer learning or synthetic data, then check on real parts |
| Lighting, dust and vibration | Control lighting and mounting first; treat model tuning as the second fix |
| Product changes | Keep a versioned dataset and a re-validation routine for each new variant |
| Integration with PLC, MES and ERP | Define the interface and failure behaviour before commissioning |
| Skills and ownership | Name an owner for thresholds, retraining and review of rejected parts |
| Cost | Start with one station and one defect class; open libraries such as OpenCV lower software cost, but the full cost includes optics, lighting and integration |
Which standards and rules apply?
| Source | What it covers | Status |
|---|---|---|
| ISO 9001:2015 | Quality management system requirements (ISO page) | Published; the ISO page lists edition 5 from September 2015 |
| ISO 10218-1:2025 | Safety requirements for industrial robots as partly completed machinery (ISO page) | Published, third edition, February 2025; Part 2:2025 covers integration into systems and applications |
| EU AI Act | Risk-based rules for AI systems; AI in products covered by EU product-safety law is treated under Annex I | Per the European Commission page, applicable from 2 August 2026 with exceptions; Annex I rules apply from 2 August 2028 |
| NIST AI Risk Management Framework | Voluntary framework for managing AI risk | AI RMF 1.0 released 26 January 2023; NIST says it is being revised |
A vision system that only flags parts for a person is a different risk from one that stops a robot or releases product. Confirm with your safety and compliance teams which rules apply to your machine, market and use. This is not legal advice.
How should a manufacturer adopt vision inspection?
| Step | Action | Exit test |
|---|---|---|
| 1. Pick one station | Choose a defect class with clear visual cues and a known cost | Defect definition agreed with quality |
| 2. Build the image set | Capture from the real line under real lighting | Reviewed and labelled by inspectors |
| 3. Run in shadow mode | Model scores parts while people still decide | Disagreements reviewed and explained |
| 4. Gate with a human | Model rejects, a person confirms borderline cases | Stable review rate |
| 5. Automate the clear cases | Let the line act on high-confidence results only | Audit sample shows no drift |
| 6. Monitor and retrain | Track drift, new variants and false rejects | Scheduled re-validation |
When not to use it: if defects are not visible, if you cannot define a good part, or if the line changes too often to keep a validated dataset, fix the process or add other sensors first.
How do you govern inspection decisions?
Record the image, model version, threshold and outcome for every decision, so a customer complaint or audit can be traced. Review rejected and escaped parts regularly and feed what you learn into thresholds and training. ElixirData's Decision Review Agent is described on its site as examining AI agents' past decisions and outcomes to find inconsistencies and recurring problems and to suggest policy or process changes. ElixirData keeps governed context, versioned policy and decision traces in one decision layer above AI agents. Where inspection feeds wider agent-driven operations, see our guide to agentic workflows.
The same discipline applies in other regulated vision settings; for a medical example, see AI-assisted medical imaging.
What will change in assembly line inspection over the next 3 to 5 years?
These points rest on published dates and standards; they are not market forecasts.
| Change | Source | What it means for inspection |
|---|---|---|
| EU AI Act application dates | European Commission AI Act page: general application from 2 August 2026; Annex I products from 2 August 2028 | Plan conformity and documentation work for vision that acts as a safety component in a regulated product |
| Updated robot safety standard | ISO 10218-1:2025 and 10218-2:2025 | Review cells where vision guides or stops robots against the new edition |
| AI risk framework revision | NIST says AI RMF 1.0 is being revised | Align governance of model changes to the framework as it evolves |
| Agent-based operations | Our view, not a sourced forecast | Inspection results are likely to trigger more automated actions, so decision logs and human review matter more |
The practical outlook: the model matters less over this period than the evidence around it, meaning data, validation, change control and review of decisions.
To map one inspection decision your line should make, and the context and policy it depends on, book a Context Workshop. See what happens in the workshop.
What should you plan for in 2027?
Vision inspection stations installed now will be judged against rules that phase in over the next two years, so keep the evidence trail ready.
- 2 December 2027: the European Commission says AI Act rules for Annex III high risk use cases, such as employment and education, will apply from this date after the AI Omnibus delay. Ask your legal team whether any of your use falls under those listed uses.
- 2 August 2028: the same page says Annex I high risk systems, meaning products such as lifts or toys covered by EU product safety law, have an extended transition period until this date. Check whether a vision system that acts as a safety component in such a product is covered.
Keep one validated intended use per model, a change control routine and a decision log. They serve whichever rule ends up applying.
Frequently asked questions
How does computer vision inspect an assembly line?
Cameras capture each part, a trained model finds defects or errors, and the line controller passes, rejects or reworks the part. The result and image are stored for traceability.
Should the model run at the edge or in the cloud?
Inference usually runs next to the line for low latency and to keep images on site, while training and fleet management often run in the cloud. The choice depends on cycle time, connectivity and data rules.
Does the EU AI Act apply to vision inspection?
It can. The European Commission page says the Act is applicable from 2 August 2026 with exceptions, and Annex I rules for AI in regulated products apply from 2 August 2028. Check your use with compliance teams; this is not legal advice.
Which standards matter for inspection and robots?
ISO 9001:2015 covers quality management systems. ISO 10218-1:2025 and 10218-2:2025 cover industrial robot safety and system integration. NIST AI RMF is a voluntary AI risk framework.
How should a manufacturer start?
Pick one station and one defect class, build an image set from the real line, run the model in shadow mode, then add a human gate before automating clear cases.
What will change in vision inspection over the next 3 to 5 years?
Published regulatory dates, an updated robot safety standard and a revised NIST framework point to more emphasis on validation, documentation and decision records.
Follow XenonStack on LinkedIn: XenonStack on LinkedIn for new guides on agentic AI, data and platform engineering.
Ready to put AI agents to work? Explore ElixirClaw, the agentic OS platform to build, orchestrate and govern AI agents.
Explore the XenonStack platform family: ElixirData · ElixirClaw · ElixirHub · NexaStack · MetaSecure · Neural AI · AgentGRC · AgentSRE · AgentAnalyst · AgentInstruct · AgentRAI · AgentScrum · AgentSearch · AgentForce · AI Aviator · SAIF Aviator · CohortIQ · XenonStack AI · XenonStack UAE