Key takeaway
- AI quality control uses cameras, edge inference and MES/QMS links to catch defects inline. Architecture, false-reject trade-offs and ISO 9001 traceability.
AI-driven quality control in manufacturing uses cameras, sensors and machine learning models, usually running at the edge next to the line, to inspect every part in real time and decide whether it passes, fails or needs a human look. The value comes less from the model and more from the loop around it: each verdict is linked to a lot, a machine state and a QMS record, so defects are contained early and every decision can be traced.
For leaders, the real choices are where to inspect, how many false rejects the line can tolerate, and how inspection evidence feeds MES, QMS and ISO 9001 traceability. This guide covers the architecture, the trade-offs, the regulation that applies, and an honest view of where AI inspection does not pay off.
What is AI-driven quality control in manufacturing?
AI-driven quality control is the use of trained models, rather than only fixed rules, to judge product and process quality. It covers three related jobs:
- Visual inspection: deep learning models classify or locate surface defects, missing parts, wrong labels or assembly errors from camera images.
- Process monitoring: models read sensor and machine data (temperature, pressure, vibration, torque, speed) to flag drift that will cause defects before they appear.
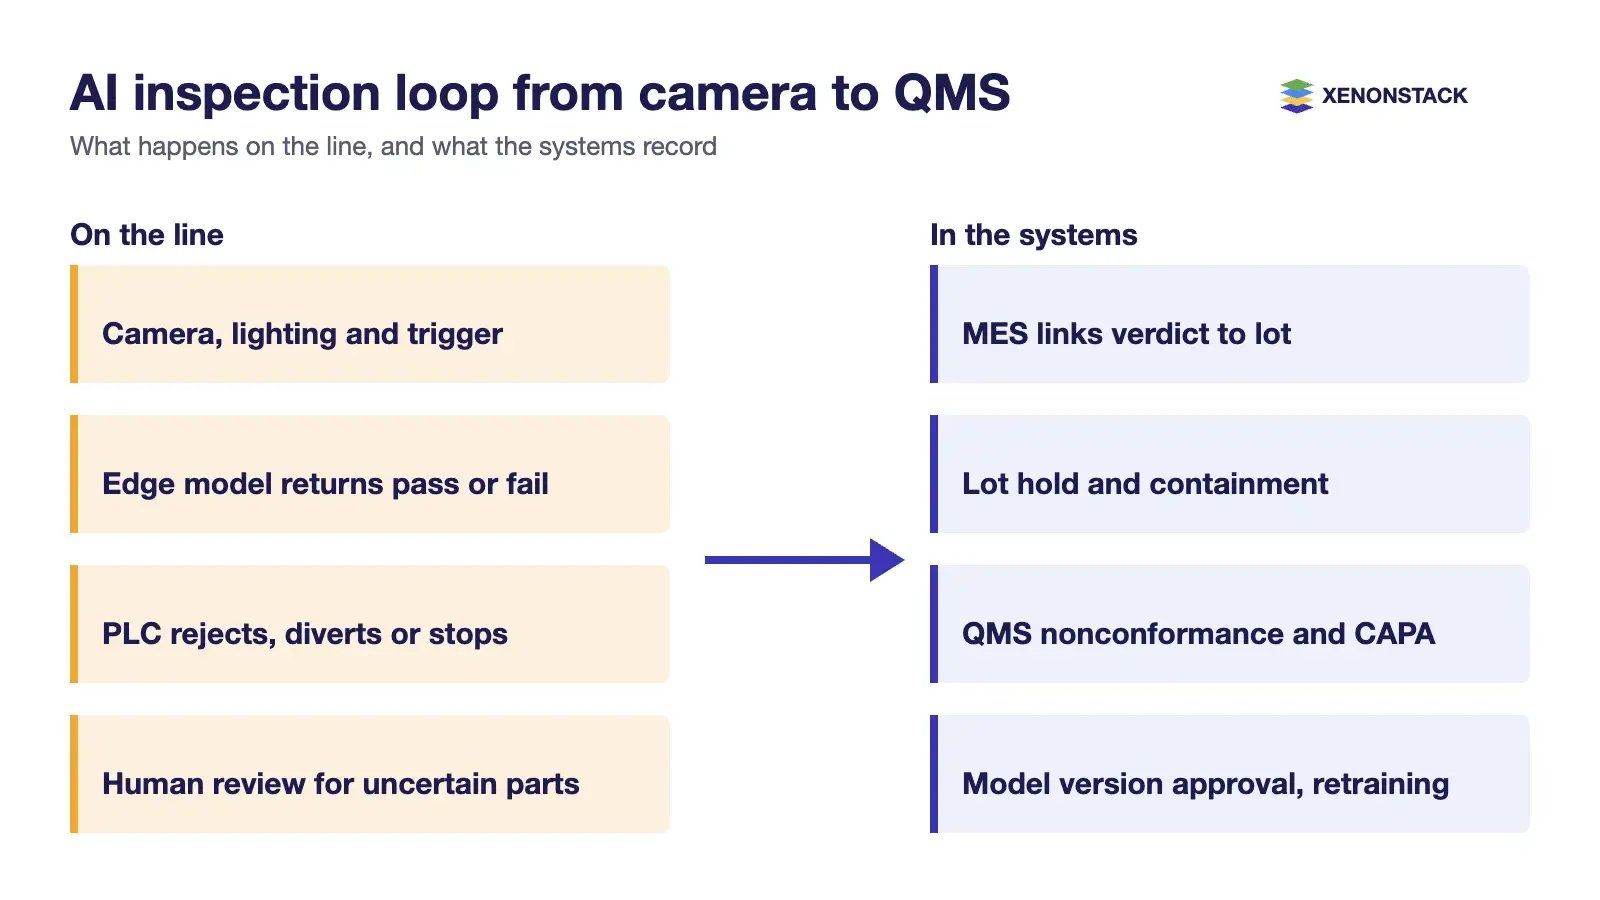
- Decision and containment: the result is turned into an action, such as reject the part, hold the lot, slow the line or raise a nonconformance, and recorded with its evidence.
Why does AI quality control matter to manufacturing leaders now?
Manual inspection does not scale with line speed, and it gets less consistent as shifts get longer. End-of-line sampling finds problems after the material, energy and machine time are already spent. Two business pressures make inline AI inspection a board-level topic:
- Cost of poor quality: scrap, rework, warranty claims and recalls grow the later a defect is found. Catching a defect at the station that caused it limits the damage to a few units instead of a pallet.
- Audit and customer evidence: automotive, medical, aerospace and food customers expect proof of inspection per lot or serial number, not a sampling plan and a signature.
The timing also matters. ISO 9001:2026 was published on 16 September 2026, with existing certificates expected to remain valid until 30 September 2029 (DQS). The EU Machinery Regulation applies from 20 January 2027. Plants that redesign inspection now can build the evidence trail both will ask for.
How is an AI inspection architecture built, from camera to MES and QMS?
A production inspection system has five layers. Most failures happen at the joins between them, not inside the model.
| Layer | What it does | Key design choices | Where it breaks |
|---|---|---|---|
| Capture | Industrial cameras, lighting, optics, triggers and sensors produce a consistent image or signal per part | Resolution vs field of view, area vs line-scan, lighting geometry, trigger from PLC or encoder | Lighting changes, dirty lenses, vibration, part position drift |
| Edge inference | Runs the model next to the line and returns a verdict within the cycle time | Industrial PC or GPU gateway, model size, latency budget, offline behaviour | Latency spikes, hardware failure, model version mismatch between lines |
| Control action | Turns the verdict into a reject, divert, alarm or line stop through the PLC | Fail-safe default if inference is unavailable, operator override | Good parts rejected or bad parts passed when timing or signals drift |
| MES integration | Links each verdict to work order, lot, serial number, machine and operator; triggers lot holds | Event model (often ISA-95 aligned), OPC UA or MQTT messaging, store-and-forward | Results without lot context, lost messages during network outages |
| QMS and model operations | Creates nonconformance records, CAPA links and evidence; manages labelling, retraining and approval of model versions | Image retention policy, label review workflow, change control for models | Unreviewed model updates, missing evidence for audits |
Why run inference at the edge?
Most lines need a verdict in milliseconds, before the part reaches the reject gate. Sending every image to a cloud service adds latency and depends on the network. Edge inference keeps the decision local, while the cloud or data centre handles training, fleet monitoring and long-term storage. Our guides to computer vision on the edge and edge AI in the smart factory cover the deployment patterns in more depth. Platforms such as NexaStack, an Agentic Operating Platform for Physical AI that runs on-premises, in cloud and hybrid, are one way to manage models across many lines and sites.
Why do MES and QMS links matter more than model accuracy?
A verdict that is not tied to a lot cannot drive a hold, and a defect that is not logged in the QMS cannot drive corrective action. The integration design decides whether AI inspection reduces escapes or just produces another dashboard. Define the event schema (part ID, station, time, model version, verdict, confidence, image link) first.
How should you balance false rejects against defect escapes?
Every inspection system trades two errors. A false reject (a good part rejected) costs yield and capacity. An escape (a bad part passed) costs warranty, customer trust and sometimes safety. The model's confidence threshold sets the balance, and the right setting depends on the cost of each error, not on a single accuracy figure.
| Situation | Lean towards | Typical control |
|---|---|---|
| Safety-critical or regulated parts (brakes, implants, aerospace fasteners) | Fewer escapes, accept more false rejects | Low threshold, all rejects go to human re-inspection |
| High-volume, low-cost consumer parts | Fewer false rejects, accept small escape risk | Higher threshold, downstream sampling audit |
| New product or new defect type | Conservative until data builds up | Shadow mode next to human inspection before automatic rejects |
Measure both errors on a held-out set from your own line, re-check them after every model change, and report them separately. A single "99% accurate" number can hide an escape rate that is too high, because defects are rare.
Which inspection approach fits which line?
There is no single best tool. Choose by defect type, data available and how often the product changes.
| Approach | Choose it when | Watch out for |
|---|---|---|
| Rule-based machine vision | Measurement, presence, barcode and alignment checks under stable conditions | Brittle with natural variation; rule sets grow hard to maintain |
| Supervised deep learning (classification, detection, segmentation) | You have labelled examples of each defect type and need to know which defect it is | Needs enough defect images; rare defects are under-represented |
| Anomaly detection trained on good parts | Defects are rare or unpredictable, but "good" is consistent | Flags any change, including harmless ones; needs a review band |
| Process-signal models (sensor and machine data) | Defects are caused by drift you can measure before the part is made | Needs clean, time-aligned data from machines and MES |
Rule-based vision still suits stable measurement checks. The difference between quality assurance and quality control matters too: AI inspection is a control, and improves assurance only when findings flow back into the process. Many plants combine these: rules for dimensions, deep learning for cosmetic defects, and process signals to explain why defects appear. When models must justify their verdicts to engineers and auditors, techniques from explainable AI in manufacturing, such as heat maps over the defect region, help build trust.
How does AI inspection support ISO 9001 traceability and regulation?
ISO 9001 asks an organisation to identify outputs, keep traceability where it is required, control nonconforming outputs and keep monitoring and measuring resources fit for purpose. In the 2015 edition these sit mainly in clauses 7.1.5, 8.5.2 and 8.7. ISO 9001:2026 keeps these themes and adds stronger expectations on quality culture and ethical conduct from top management (DQS summary; ISO 9001 at ISO). For AI inspection this means:
- The model is a measuring resource. Treat it like a gauge: a defined validation method, an approved version, and re-validation after changes.
- Every verdict is a record. Store part or lot ID, model version, threshold, result and image reference, for the retention period your customers require.
- Nonconformances close the loop. Rejects and holds should open QMS records automatically, with human disposition and corrective action.
In the EU, Regulation (EU) 2023/1230 on machinery applies from 20 January 2027. It expects AI-enabled machinery to operate within limits set by the manufacturer, to record data on safety-critical decisions, and to let operators intervene; machinery with machine-learning-based safety functions needs a notified body (UL Solutions). The Digital Omnibus on AI, Regulation (EU) 2026/1744, in force since 27 July 2026, moves machinery to a sectoral approach under the Machinery Regulation and sets 2 August 2028 for AI Act obligations on AI in products under EU product law (EUR-Lex; DLA Piper). Most quality inspection is not a safety function, but if a vision system guards people or stops a hazardous machine, take legal advice early.
The governance gap is usually not the model but the decision around it: who approved the threshold, which policy said a lot should be held, and why an override was accepted. ElixirData keeps governed context, versioned policy and decision traces in one decision layer above the agents, and its audit agent is one way to assemble that evidence for quality audits.
How do you adopt AI quality control and measure success?
- Pick one station with a known cost of poor quality. Choose a defect that is visible, frequent enough to learn from, and expensive when it escapes.
- Fix capture first. Stable lighting, fixturing and triggering often matter more than the model choice.
- Run in shadow mode. Compare model verdicts with human inspection for several weeks, across shifts and material batches.
- Integrate before scaling. Connect verdicts to MES lot holds and QMS nonconformances, then switch on automatic rejects with a review band.
- Industrialise model operations. Label review, retraining triggers, version approval and rollback, managed the same way across lines. Link findings to predictive maintenance where machine condition drives defects.
| Metric | What it tells you |
|---|---|
| Escape rate (defects found downstream or by customers) | Whether inspection is protecting the customer |
| False reject rate and re-inspection load | Yield cost and reviewer workload |
| First pass yield and scrap cost per unit | Business impact of earlier detection |
| Time from defect to containment (lot hold) | How well MES integration works |
| Share of verdicts with full traceability record | Audit readiness |
When is AI quality control not the answer?
- When a rule or gauge already works. Simple dimensional or presence checks rarely need deep learning.
- When the defect is not observable. Internal flaws may need X-ray, ultrasound or destructive testing; a surface camera will not find them.
- When capture cannot be stabilised. If lighting, part position or surface finish vary without control, fix the station first.
- When there is no owner for the loop. Without someone to review rejects, approve model changes and act on root causes, accuracy decays and trust goes with it.
- When volumes are very low. For bespoke or low-volume parts, skilled human inspection with good tooling may cost less.
What will change in AI-driven quality control over the next 3 to 5 years?
- From detection to agents that act. Inspection will combine the image with machine and process signals to decide on holds and adjustments, not just flag defects, with small models running at the line (World Economic Forum, June 2026). Gartner forecasts that industrial AI agents from AIoT platform providers will rise from about 3% to 65% production use in asset-intensive industries by 2030 (Virtualization Review, reporting Gartner). See our view of agentic AI in manufacturing.
- More automation of quality processes. PwC research reports that the share of industrial manufacturers expecting to highly automate key processes by 2030 will rise from 18% to 50% (ICTbusiness, reporting PwC).
- Decision evidence as a requirement. From January 2027 in the EU, machinery rules expect records of safety-critical decisions and operator intervention, and AI Act duties for AI in regulated products follow from August 2028. Expect customers to ask for the same evidence on quality decisions.
To map one decision your agents should make, and the context and policy it depends on, book a Context Workshop. See what happens in the workshop.
Frequently asked questions
What is AI-driven quality control in manufacturing?
It is the use of cameras, sensors and machine learning models, usually at the edge, to inspect parts and processes in real time and decide whether to pass, reject or send a part for human review, with each verdict recorded for traceability.
Why should AI inspection run at the edge?
Most lines need a verdict within the cycle time, before the part reaches the reject gate. Edge inference keeps that decision local and independent of the network, while training and fleet monitoring run centrally.
How do you balance false rejects and defect escapes?
Set the model threshold by the cost of each error. Safety-critical parts favour fewer escapes and more re-inspection; high-volume, low-cost parts favour fewer false rejects. A review band that sends uncertain parts to a human helps in both cases.
How does AI inspection support ISO 9001 traceability?
Treat the model as a measuring resource with an approved version and validation, record every verdict against a part or lot with the model version and image reference, and open QMS nonconformance records automatically for rejects and holds.
Does the EU Machinery Regulation apply to AI quality inspection?
Regulation (EU) 2023/1230 applies from 20 January 2027. Most quality inspection is not a safety function, but if a vision system protects people or stops hazardous machinery, its requirements on recorded decisions, operator intervention and notified body assessment can apply.
When is AI quality control not worth it?
When a simple rule or gauge already works, when the defect cannot be seen by the sensor, when capture conditions cannot be stabilised, when volumes are very low, or when no one owns review and model changes.
Follow XenonStack on LinkedIn: XenonStack on LinkedIn for new guides on agentic AI, data and platform engineering.
Ready to put AI agents to work? Explore ElixirClaw, the agentic OS platform to build, orchestrate and govern AI agents.
Explore the XenonStack platform family: ElixirData · ElixirClaw · ElixirHub · NexaStack · MetaSecure · Neural AI · AgentGRC · AgentSRE · AgentAnalyst · AgentInstruct · AgentRAI · AgentScrum · AgentSearch · AgentForce · AI Aviator · SAIF Aviator · CohortIQ · XenonStack AI · XenonStack UAE