Key takeaway
- Enterprise manufacturing intelligence in 2027: what EMI does, ISA-95 data sources, use cases, current platforms, OT security and an adoption plan.
Enterprise manufacturing intelligence (EMI) is software that pulls data from plant-floor and business systems, such as PLCs, SCADA, historians, MES and ERP, puts it into one context and turns it into views, alerts and decisions that operations and business leaders can act on. It sits above control systems, reads from them, and answers questions no single system can answer on its own: why a line lost output, which supplier lot drives scrap, or what a shift really costs in energy.
In 2026 the building blocks have changed. Edge data planes speak OPC UA and MQTT, cloud services now offer real-time manufacturing analytics, several older IoT services have retired, and AI agents are starting to query plant data directly. The value of EMI now depends less on dashboards and more on a clean, governed data model that people and agents can both trust.
What is enterprise manufacturing intelligence?
EMI is a layer of manufacturing analytics that combines operational technology (OT) data with information technology (IT) data across one or many sites. Where a manufacturing execution system runs the work on a line, EMI explains the work: it correlates events, compares plants, and tracks performance against cost, quality and delivery targets. It reads from existing systems rather than replacing them, which is why it is usually adopted after MES and ERP are in place.
| System | What it does | When it fits |
| Historian | Stores high-frequency time-series tags from control systems | You need process history for one site or unit |
| MES | Runs and records production orders, routing, genealogy and quality checks | You need to execute and trace work on the shop floor |
| Business intelligence (BI) | Reports on business data, mostly from ERP and finance | You need financial and commercial reporting |
| Enterprise manufacturing intelligence | Joins OT and IT data in context and compares lines, plants and periods | You run several lines or sites and need one operational view tied to cost and quality |
Which data sources does an EMI system combine?
Most EMI designs follow the ISA-95 standard, also known as IEC 62264. ISA-95 describes five levels, from the physical process at level 0 to business planning and logistics at level 4, and it mainly deals with the interface between level 3 (manufacturing operations management, including MES) and level 4 (business systems such as ERP). EMI reads across all of these levels, so the ISA-95 model is a practical way to scope what to connect first.
| ISA-95 level | Typical systems | What EMI uses from it |
| Levels 0 and 1 | Machines, sensors, valves, smart devices, IIoT sensors | Condition, energy and process signals |
| Level 2 | PLCs, DCS, SCADA, historians | Machine states, alarms, cycle data and setpoints |
| Level 3 | MES, quality and maintenance systems | Orders, batches, genealogy, inspections and work orders |
| Level 4 | ERP, supply chain and finance systems | Materials, standard costs, demand and supplier data |
The hard part is context, not storage. A temperature tag only becomes useful when it is linked to an asset, an order, a batch and a cost. That is why current platforms ship asset models and data contracts, and why edge data management decisions, such as what to filter, buffer and keep on site, shape the quality of every report built on top.
What has changed in manufacturing intelligence since 2023?
Three shifts matter for leaders planning EMI today. First, open protocols now carry plant data to the analytics layer. OPC UA is used to read from equipment, and MQTT with the Eclipse Sparkplug specification, now at version 3.0, adds birth and death certificates so subscribers know whether data is current. Many teams use this pattern to build a shared namespace that every application subscribes to. Second, hyperscalers offer packaged manufacturing data services. Third, some services have retired, so older EMI designs need a migration plan.
| Service | What it does | Current status (checked 11 Nov 2026) |
| Azure IoT Operations | Edge data plane on Azure Arc-enabled Kubernetes with an MQTT broker, an OPC UA connector and data flows that transform and contextualise data | Current |
| Fabric Real-Time Intelligence | Eventstreams, Eventhouse (KQL), Real-Time dashboards, Activator alerts and data agents over live and historical data | Current; digital twin builder is in preview |
| AWS IoT SiteWise | Collects, stores, organises and monitors industrial equipment data with asset models; SiteWise Edge processes data on site and connects up to 100 OPC UA servers per gateway | Current |
| Google Manufacturing Data Engine | Packaged solution that unifies edge telemetry with ERP data; Manufacturing Connect, built by Litmus, is the edge gateway | Current; Google describes quality, maintenance and scheduling agents on this data foundation |
| Azure IoT Central | Managed IoT application platform | No new applications from 23 September 2026; existing applications work until 20 September 2029. Microsoft recommends IoT Hub with DPS and Microsoft Fabric |
| Amazon Lookout for Equipment | Equipment anomaly detection | AWS discontinued support on 7 October 2026; the console and resources are no longer accessible |
For a wider view of these platform changes, see our guide to industrial IoT applications. Where EMI has to run close to machines across on-premises, cloud and hybrid sites, NexaStack is an agentic operating platform for physical AI that runs across those environments.
What are the main use cases of enterprise manufacturing intelligence?
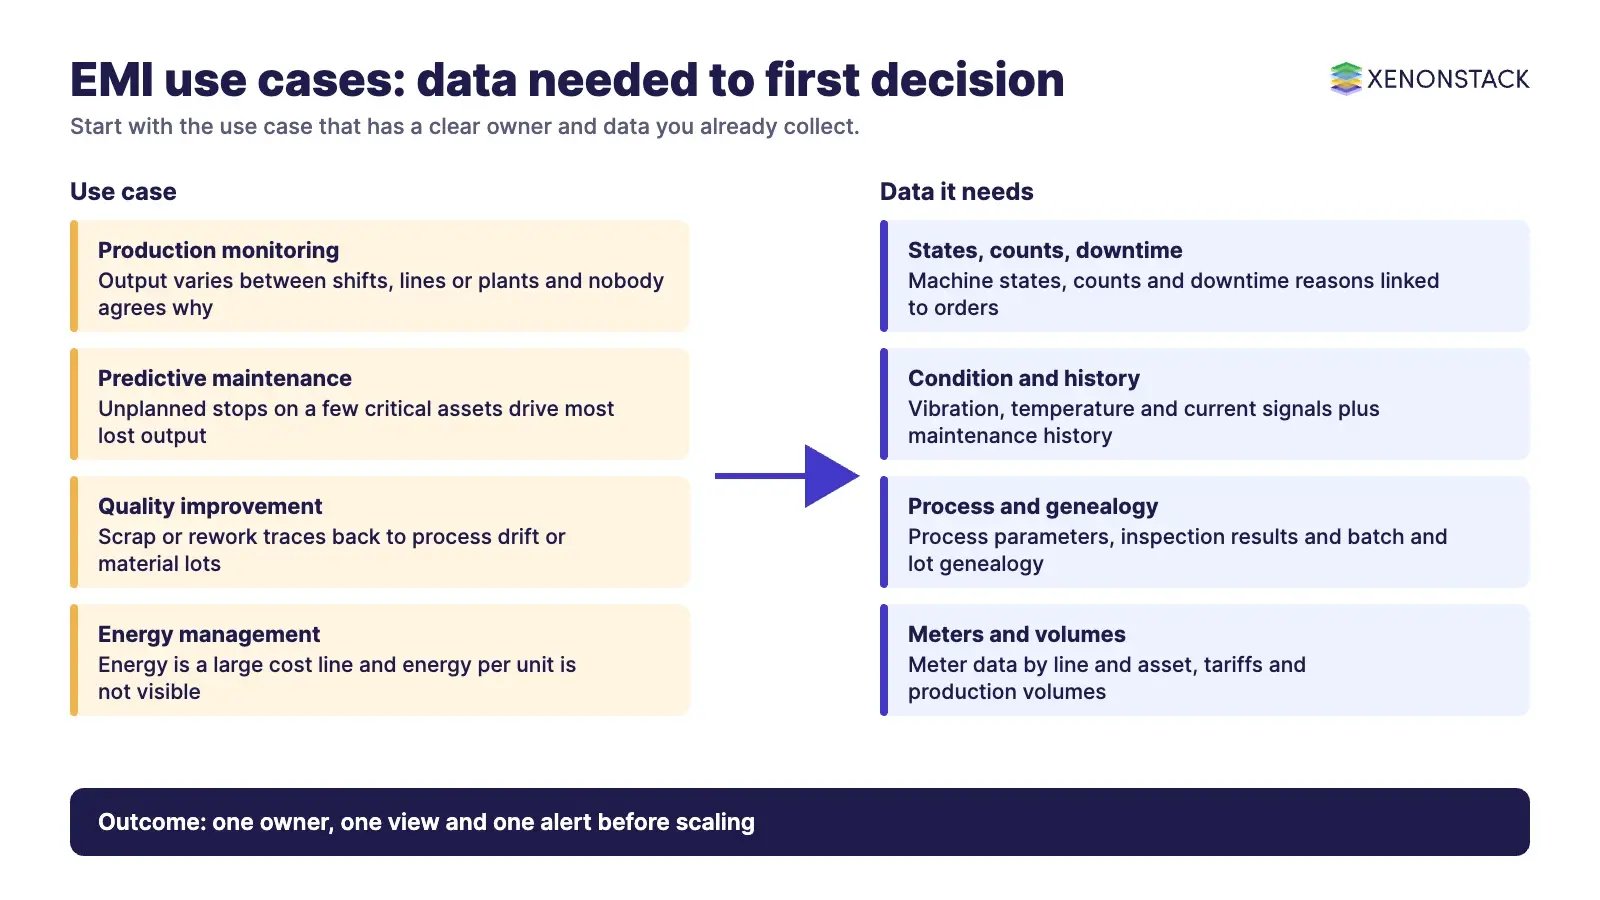
Start with the use case that has a clear owner and data you already collect. The table below shows the common EMI use cases, the data each one needs and when it is the right first step.
| Use case | Data it needs | When it fits first |
| Production monitoring | Machine states, counts, downtime reasons, order data | Output varies between shifts, lines or plants and nobody agrees why |
| Predictive maintenance | Vibration, temperature and current signals, maintenance history | Unplanned stops on a few critical assets drive most lost output |
| Quality control and improvement | Process parameters, inspection results, batch and lot genealogy | Scrap, rework or complaints trace back to process drift or material lots |
| Supply chain and production planning | Inventory, supplier delivery, demand and capacity data | Schedules break because material or capacity data is late or wrong |
| Energy management | Meter data by line and asset, tariffs, production volumes | Energy is a large cost line and you cannot see energy per unit |
| Process optimisation | Setpoints, recipes, outcomes and quality data | You have stable monitoring and want to tune the process itself |
Production monitoring
Real-time monitoring is the most common first use case. EMI collects machine states, counts and downtime reasons, links them to orders, and shows throughput, cycle time and scrap by line, shift and product. Alerts flag deviations while they can still be fixed, and the same data supports comparisons across plants.
Predictive maintenance
Predictive maintenance uses condition data and maintenance history to estimate when equipment is likely to fail, so work can be planned rather than forced by a breakdown. Because some managed anomaly-detection services have retired, many teams now keep these models on their own ML platform. Our predictive maintenance with machine learning use case shows the approach in more detail.
Quality control and improvement
EMI links process parameters to inspection results and batch genealogy. That lets quality teams see which process step, machine or material lot drives defects, and set alerts when a parameter drifts towards the limit rather than after scrap appears.
Supply chain and production planning
By joining inventory, supplier performance and shop-floor capacity, EMI helps planners adjust schedules to real conditions, for example when a critical component runs low or a machine is down. Integration with MES and ERP keeps plans and execution aligned.
Energy management
Meter data by line and asset, combined with production volumes, gives energy per unit. That shows which machines or shifts use energy inefficiently and supports both cost and sustainability reporting.
Process optimisation and workforce skills
Once monitoring is stable, the same data can tune setpoints and recipes, and show where operators need training on specific machines or processes. Our manufacturing data analytics platform use case describes how these analytics come together on one platform.
Which tools and techniques power manufacturing analytics today?
Classic intelligent manufacturing research relied on fuzzy logic, genetic algorithms, neural networks and case-based reasoning. These techniques are still in use, but they now sit next to machine learning and generative AI agents. Choose by problem, not by trend.
| Technique | What it does | When it fits |
| Rules and statistical process control | Thresholds, control limits and alarms on known parameters | Well-understood processes where explainability matters most |
| Fuzzy logic control | Encodes operator experience as rules such as high, medium and low | Processes run by expert judgement that is hard to model exactly |
| Genetic algorithms and optimisation | Search large solution spaces, for example schedules or assembly sequences | Scheduling and planning problems with many conflicting constraints |
| Case-based reasoning | Reuses past problems and solutions to interpret new situations | Troubleshooting where a library of past cases exists |
| Machine learning | Learns patterns for anomaly detection, failure prediction and quality prediction | Enough labelled history exists and the signal is not captured by rules |
| AI agents over governed data | Answer questions and trigger actions using live and historical plant data | The data model is clean, access is controlled and a person approves actions |
Agents are the newest layer. Fabric Real-Time Intelligence data agents can reason over live and historical Eventhouse data, and Google describes quality, maintenance and scheduling agents built on Manufacturing Data Engine. To let plant and business teams ask questions in plain language, AgentAnalyst lets teams ask questions of enterprise data in plain language and get real-time insights.
How should you govern and secure manufacturing intelligence?
EMI connects OT and IT networks, so security has to be designed in from the start. The ISA/IEC 62443 series sets requirements and processes for securing industrial automation and control systems, with shared responsibilities across asset owners, product suppliers, integrators and service suppliers. NIST SP 800-82 Rev. 3, the Guide to Operational Technology Security (September 2023), describes OT threats and recommended countermeasures; NIST has released an initial public draft of Revision 4, with comments due on 30 November 2026.
- Read by default: EMI should read from control systems. Any write-back to setpoints or schedules needs an approval step and an audit trail.
- Access by role: plant, corporate and partner users see only the assets and sites they are responsible for.
- Data contracts: each tag and table has an owner, units and a definition, so a KPI means the same thing in every plant.
- Cost control: filter and aggregate at the edge, and keep raw high-frequency data only where a use case needs it, to keep cloud ingestion and storage costs predictable.
- Agent guardrails: when agents read plant data or propose actions, record which data and policy each decision used. ElixirData Context OS keeps governed context, versioned policy and decision traces in one decision layer above AI agents.
How do you adopt enterprise manufacturing intelligence step by step?
- Pick one decision and one owner. For example, reduce unplanned downtime on a bottleneck line, owned by the plant manager.
- Map the data with ISA-95. List the level 0 to level 4 sources the decision needs and who owns each one.
- Connect at the edge on open standards. Use OPC UA to read equipment and MQTT to publish into a shared namespace, with buffering for network outages.
- Model assets and KPIs once. Define assets, hierarchies and KPI formulas in one model that every site reuses.
- Deliver one view and one alert. Ship a working dashboard and alert for the chosen decision before adding more.
- Add prediction and agents after the basics work. Introduce ML models and AI agents once the data is trusted, with human approval for any action on the plant.
- Scale to the next line and site. Reuse the model, connectors and security pattern, and compare sites on the same definitions.
For how agentic AI is applied once these foundations are in place, see our page on agentic AI for manufacturing and the IoT solutions for smart manufacturing use case.
What are the trade-offs, and when is EMI not the right investment?
| Choice | Benefit | Trade-off |
| Packaged cloud service | Faster start with ready asset models and connectors | Closer ties to one vendor; check lifecycle notices, as retirements show |
| Open-standard, build-your-own stack | Portability across vendors and sites | More engineering and operations effort |
| Edge-heavy processing | Lower latency, works offline, less data leaves the plant | More hardware and software to manage on each site |
| Cloud-heavy processing | Easier cross-site comparison and AI at scale | Depends on connectivity; ingestion and storage costs grow with data volume |
EMI is not the right first investment if a single site has no MES or reliable machine data yet, if the main problem is a missing ERP process rather than missing insight, or if no one owns the decisions the dashboards would inform. In those cases, fix data capture and ownership first.
To map one manufacturing decision your agents should make, and the plant data and policy it depends on, book a Context Workshop. See what happens in the workshop.
What should you plan for in 2027?
The foundations in this guide matter more than any single tool as plans are set for the next year.
- Keep one decision and one owner. Start with a single use case on a bottleneck line and ship one view and one alert before adding more.
- Treat vendor lifecycle notices as a standing review. Packaged cloud services bring faster starts but closer ties to one vendor, and several have already retired, so keep an exit route and an open standards connection layer.
- Add agents only on governed data. Introduce prediction and AI agents once the data model is trusted, with read by default access, an approval step and an audit trail for any action on the plant.
Frequently asked questions
What is the difference between EMI and MES?
An MES runs and records work on the shop floor, such as orders, routing and genealogy. EMI reads from MES, control systems and ERP, joins the data in context and analyses performance across lines and sites. EMI usually builds on an MES rather than replacing it.
Which standard should we use to structure EMI data?
ISA-95, also known as IEC 62264, is the common reference. It describes five levels from the physical process to business planning and mainly covers the interface between manufacturing operations (level 3) and business systems (level 4).
Which cloud services for manufacturing data have retired?
Azure IoT Central stopped new application creation on 23 September 2026, and existing applications work until 20 September 2029. AWS discontinued support for Amazon Lookout for Equipment on 7 October 2026.
Can AI agents use manufacturing intelligence data?
Yes. Fabric Real-Time Intelligence data agents can reason over live and historical Eventhouse data, and Google describes quality, maintenance and scheduling agents on Manufacturing Data Engine. Agents work best on a clean, governed data model with human approval for any action on the plant.
Which security standards apply to EMI?
The ISA/IEC 62443 series covers security for industrial automation and control systems, and NIST SP 800-82 Rev. 3 is a guide to operational technology security. NIST has released a draft of Revision 4 for public comment.
Follow XenonStack on LinkedIn: XenonStack on LinkedIn for new guides on agentic AI, data and platform engineering.
Ready to put AI agents to work? Explore ElixirClaw, the agentic OS platform to build, orchestrate and govern AI agents.
Explore the XenonStack platform family: ElixirData · ElixirClaw · ElixirHub · NexaStack · MetaSecure · Neural AI · AgentGRC · AgentSRE · AgentAnalyst · AgentInstruct · AgentRAI · AgentScrum · AgentSearch · AgentForce · AI Aviator · SAIF Aviator · CohortIQ · XenonStack AI · XenonStack UAE